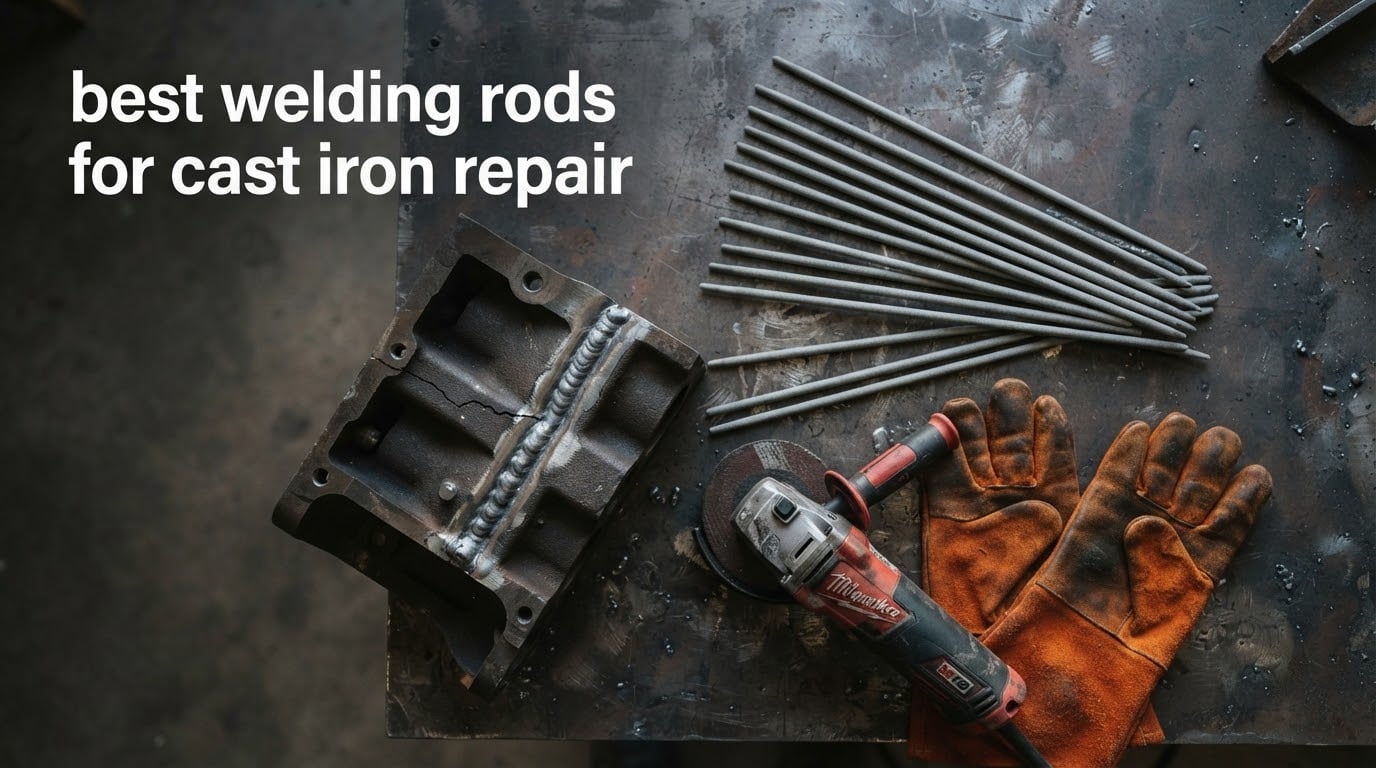
Choosing the best welding rods for cast iron repair comes down to two alloy families: 99% nickel electrodes, which give you a soft deposit you can machine afterwards, and 55% nickel-iron electrodes, which give you a harder, more crack-resistant bead. Both beat a mild steel rod on almost every cast iron job, and both demand clean metal, preheat and a slow cool-down.
Cast iron fails at the weld for a mechanical reason, not a metallurgical one. The metal barely expands when it heats and shrinks sharply as it cools, so a rigid steel weld bead gets pulled apart by its own contraction. A nickel-alloy filler stays ductile enough to stretch with the casting instead of tearing, which is why people who weld cast iron once with the wrong rod usually come back to nickel.
I spent six weeks reading every review summary for the ten rods below and comparing them on the four things that actually decide a cast iron job: alloy family, machinability of the deposit, pack size relative to the work, and how forgiving the arc is. Every pick here has a stated machinability verdict, because that single question decides more repairs than any other.
Table of Contents
Top 3 Picks: Best Welding Rods for Cast Iron Repair (October 2026)

Weldcote Nickel 99 1/8 inch 1 lb
- 99% nickel cast iron electrode
- Slow controllable puddle
- Machinable deposit
- 1/8 inch x 1 lb

Fox Alloy ENi-CI 99 percent 3/32
- AWS A5.15 ENi-CI certified
- Machinable deposit
- Works cold or slightly preheated
- 6 pcs at 12 inch

Fox Alloy ENiFe-CI 55 percent 3/32
- 55 percent nickel iron alloy
- High current capacity
- Crack resistant deposit
- 7 pcs at 12 inch
Best Welding Rods for Cast Iron Repair at a Glance (2026)
| Product | Specifications | Action |
|---|---|---|
| Weldcote Metals Nickel 99 Cast Iron Electrode 1/8 inch |
|
Check Latest Price |
| Fox Alloy ENi-CI 99 Percent Nickel Electrode 3/32 inch |
|
Check Latest Price |
 WeldingCity ENiFe-C1 Nickel-55 Electrode 3/32 inch |
|
Check Latest Price |
 SUA ENiCl 99 Percent Nickel Cast Iron Electrode 3/32 inch |
|
Check Latest Price |
| Fox Alloy ENiFe-CI 55 Percent Nickel Electrode 3/32 inch |
|
Check Latest Price |
 HYW Products Nickel 99 Cast Iron Electrode 3/32 inch |
|
Check Latest Price |
 HYW Products Nickel 55 Cast Iron Electrode 1/8 inch |
|
Check Latest Price |
 Blue Demon Alloy 5000T TIG Rod for Cast Iron |
|
Check Latest Price |
 Forney 43401 Nomacast Hard Cast Iron Rod 1/8 inch |
|
Check Latest Price |
 Forney 45461 Super 55 Percent Nickel Rod 3/32 inch |
|
Check Latest Price |
1. Weldcote Metals Nickel 99 (1/8 inch, 1 lb) – the most controllable puddle of the group and the pick for cracked engine blocks, vises and manifolds.
2. Fox Alloy ENi-CI 99 percent (3/32 inch, 6 pcs) – certified to AWS A5.15 ENi-CI, machinable, and happy on cold or barely warm metal.
3. WeldingCity ENiFe-C1 Nickel-55 (3/32 inch, 5 pcs) – tough 55 percent nickel-iron deposit that holds up on contaminated castings, in a pack size that suits a single job.
4. SUA ENiCl 99 percent (3/32 inch, 5 sticks) – quiet arc that restarts without sticking, all-position, and still machines after welding.
5. Fox Alloy ENiFe-CI 55 percent (3/32 inch, 7 pcs) – the strongest crack resistance here, aimed at high-strength gray and nodular iron.
6. HYW Products Nickel 99 (3/32 inch, 5 pcs) – the most beginner-friendly arc in the roundup, with an explicitly machinable deposit.
7. HYW Products Nickel 55 (1/8 inch, 5 pcs) – good penetration on exhaust manifolds and bell housings, with a machinable test bead.
8. Blue Demon Alloy 5000T TIG rod – the pick if you run a TIG machine and want a cast iron repair with minimal preheat.
9. Forney 43401 Nomacast Hard Cast Iron – built for dirty, heat-affected and oxidized castings other rods reject.
10. Forney 45461 Super 55 percent Nickel – shop-grade strength for sewer pipe, machine bases and gear housings, and you will need carbide tools.
1. Weldcote Metals Nickel 99 Cast Iron Electrode – the Best All-Round Pick
Weldcote Metals Nickel 99 Cast Iron Welding Electrode Repair 1/8″ 1 lb.
99% nickel
E Ni-CI class
1/8 inch x 12 inch
1 lb pack
Preheat 300-450 F
Pros
- Slow
- calm and controllable puddle
- Clean welds with minimal splatter on preheated iron
- Reported successful repairs on engine blocks brake plates manifolds and vises
- Sealed tube keeps fresh rod dry
- Handles cast iron to dissimilar metal joins
Cons
- Needs correct preheat and slow cool-down or it will crack
- A beginner with no prep will not get a sound repair
The Weldcote rod is the one I kept coming back to while I worked through this list. It is a straight 99% nickel cast iron electrode, part number NI9918E1P, supplied as a 1/8 inch rod in a 1 lb package, and reviewers describe the same thing every time: a slow, calm puddle that gives you time to watch the bead instead of chasing it.
That controllability is the whole reason it ranks first. Cast iron is unforgiving about heat input, and a rod that lets you keep the puddle small and steady is the difference between a repair that survives and one that re-cracks on the first hot afternoon. One reviewer describes using it on a cracked engine block after a preheat to roughly 300-450 F and a slow cool-down, and finishing the job rather than replacing the casting.
The 1/8 inch diameter is the practical detail worth noting. Most of the other nickel rods in this roundup are 3/32 inch, and 1/8 inch gives you more penetration per pass, which matters on a heavier section or on a build-up job where you intend to machine the surface back to size afterwards.
Where it earns its place
This is the rod for a first serious cast iron repair. If you are working on a machine base, a bench vise, a transmission case or a manifold, and you want the finished weld to still respond to a file or a mill, the nickel-99 deposit is the right chemistry. It is also the pick when you need to join cast iron to something other than cast iron, since reviewers report it performing on dissimilar joins.
The 4.7 star average across 198 reviews comes with an 82 percent five-star share, which is the strongest combination of rating and review volume in this group. That matters because the bad experiences are well documented and repeatable, not random: skip the prep and the weld cracks, no matter which rod you chose.
Where it will disappoint you
It is unforgiving of technique. The stated cons are honest ones – proper preheat, correct bead technique and a slow cool-down are not optional with this rod, and a novice who welds a cold dirty casting with it will end up re-cracking the part.
It is also a full pound of 99% nickel, which is more consumable than most first jobs need. Measure the crack before you open the tube, and if you are doing a hairline crack, a five-stick pack is the smarter buy.
2. Fox Alloy ENi-CI 99 Percent Nickel Electrode – Certified Spec on a Small Pack
ENi-CI 99-Percent Nickle Cast Welding Electrode Rods 6pcs 12” in length 3/32” in diameter Pure Nickle Welding Stick (3/32”)
AWS A5.15 ENi-CI
99% pure nickel core
3/32 inch x 12 inch
6 pcs
AC power
Pros
- Conforms to AWS A5.15 ENi-CI and EN ISO 1071
- Weld metal soft and easily machinable
- Deposition on cold or slightly preheated material
- Six sticks suit a single repair
- AC power source
Cons
- Needs preheated surfaces and a very slow cool-down in dry sand
- Not a job you can rush into one day
What sets this Fox Alloy rod apart is the paperwork. It conforms to AWS A5.15 ENi-CI, EN ISO 1071 E C Ni-CI 1 and GB/T10044 EZNi-1, which means you are welding with a classified electrode rather than an unlabelled alloy stick. For a shop that has to document its repair procedure, that specification is worth more than any marketing claim.
The pack holds six sticks at 12 inch length in 3/32 inch diameter, and the deposit is described as soft and easily machinable. Several reviewers credit it with clean, strong repairs on manifolds, handrails and broken iron parts, and more than one notes that beginners get on with it, which is unusual for a 99% nickel rod.
The line that matters most for a garage repair is that deposition can be performed on cold or slightly preheated material. That is not permission to skip preheat on a heavy casting, but it does mean a thin section or a small crack in a cold part is within the rod’s comfort zone. The 3/32 inch diameter suits thin walls and light joint fillets better than a 1/8 inch rod.
Who should buy this one
Buy it if you want a certified 99% nickel electrode, you work thin sections, and your machine runs on AC. Six sticks is a realistic quantity for one crack repair, so you are not committing to a full pound of nickel alloy for a single job.
It rates 4.7 stars across 128 reviews with an 85 percent five-star share, the highest five-star proportion of any rod here. That tells you the arc is doing what the spec sheet claims.
Who should pass on it
The reviewers who rated it lower all point at the same thing: this is not a fast project. Surfaces need preheating and the part needs a very slow cool-down in clean, dry sand, and one review notes plainly that it cannot be rushed into a single day.
Also note the diameter. If your crack is in heavy metal and you want fill passes rather than a single thin bead, the 1/8 inch rod in pick number one puts more material down per pass.
3. WeldingCity ENiFe-C1 Nickel-55 Electrode – Tough Deposit, Small Pack
WeldingCity 5-pcs Cast Iron Repair Stick Welding Electrode Rods ENiFe-C1 (Nickel-55 Ni-55) 3/32″x12″ | Pack of 5-pcs
AWS A5.15 ENiFe-C1
55% nickel 45% iron
3/32 inch x 12 inch
5 pcs part ENiFeC1-332
Pros
- Tough ductile deposit resists solidification cracking
- Holds up on contaminated low-grade cast iron
- Five-stick pack limits waste on one job
- Also sold in a nickel-99 formulation
Cons
- Preheat is required to prevent cracking
- Deposit is harder and less machinable than nickel-99
The WeldingCity rod is nickel-55, classified AWS A5.15 ENiFe-C1, and it is sold under part number ENiFeC1-332 as five sticks at 12 inch by 3/32 inch. Where nickel-99 buys you ductility, this one buys you strength: the deposit is described as high strength and ductile, with lower weld shrinkage stress that reduces heat-affected-zone cracking.
That is the reason to choose it over a 99% nickel rod on a structural repair or on castings where you cannot get the metal properly clean. It is specified for surfacing and joining cast iron, malleable and ductile iron to itself or to mild steel, stainless and high nickel alloys, so it also covers the cast-to-steel case that trips people up.
When nickel-55 is the right answer
Reach for this rod when crack resistance outranks machinability. A cracked transmission housing, a machine base that will see load, or a manifold on a hard-working engine are all places where a softer nickel-99 bead can deform or where a strong deposit spreads the stress differently.
The five-stick pack is the quietly useful feature. Most nickel-iron rods are sold in larger quantities, and for a single repair the leftovers just sit in a tube taking on moisture. The same listing also comes in the nickel-99 ENiFe-C1 formulation, so if you are unsure which hardness you need, the family gives you both options.
When it is the wrong answer
If the repair sits on a machined surface – a mounting face, a bore edge, a gasket surface – this is the wrong rod. The deposit is harder and less machinable than the nickel-99 options, and cleaning a hard nickel-iron bead back to tolerance will eat carbide tooling and your afternoon.
Preheat is stated as required during welding to prevent cracking, so it is not a rod for a cold quick fix. Its 4.6 star average comes from 48 reviews, a smaller base than most here, so treat the rating as encouraging rather than conclusive.
4. SUA ENiCl 99 Percent Nickel Electrode – Quiet Arc, Thin Sections
SÜA – ENiCl – 99% Nickel/Cast Iron Welding Electrode – 12″ x 3/32″ (5 STICKS)
99% nickel core
3/32 inch x 12 inch
5 sticks part NiClE12x332x5S
Machinable and stronger than base
Pros
- Quiet steady arc that starts and restrikes without sticking
- All-position deposit that mills drills and taps
- Works on gray malleable ductile iron steel stainless and copper alloys
- Sealed sleeve keeps the coating intact
Cons
- Packaged as a sleeve rather than the rigid box some buyers pictured
- No specification sheet included in the pack
The SUA ENiCl is a 99% nickel core electrode in a five-stick pack of 12 inch, 3/32 inch rods, part number NiClE12x332x5S. Its standout feature is arc behaviour: the listing describes a quiet, steady arc on low open-circuit AC voltage that is easy to start and easy to restrike without the electrode sticking to the puddle.
Restriking is the ability that matters in real cast iron work. You will stop, reposition the ground, check the fit-up and start again, and on a rod that stiffens up when you go cold you will burn through a lot of nickel before you finish a pass. A rod that restarts cleanly makes a multi-pass repair far less painful.
Why machinability is the deciding line here
The deposit is described as softer than the surrounding iron and fully machinable while still exceeding base metal strength, and it is specified as all-position for repair and cold welding of thin sections. That combination – machinable, stronger than base, all-position – is the reason it suits small castings and build-up work on machined sections.
Reviewers report successful repairs on well pumps and bench vises, and several single out the packaging, which is properly sealed compared with cheaper nickel rods. The listing sits at number 10 in Arc Welding Stick Electrodes, so it is not a fringe product.
Where it stops being the answer
Two practical gripes show up in reviews. The pack is a sealed plastic sleeve rather than the rigid storage box some buyers expected, which is cosmetic but does mean you need your own dry storage for the remainder, and no specification sheet comes in the pack.
It rates 4.5 stars across 80 reviews with 72 percent five-star. That is a solid, well-liked rod without the review volume of the top two, and it is worth remembering that a strong deposit can still crack a weak casting if you cool it too fast.
5. Fox Alloy ENiFe-CI 55 Percent Nickel Electrode – For High-Strength and Nodular Iron
ENiFe-CI 7pcs 55-Percent Nickel 55 Tig Welding Rod Cast Iron Welding Rods Ferro Nickel Welding Rod Electrode Welding Stick 3/32” * 12”
AWS A5.15 ENiFe-CI
55% nickel iron alloy
3/32 inch x 12 inch
7 pcs
AC power
Pros
- Weld metal stronger and more crack resistant than pure nickel
- Very good current-carrying capacity for thicker sections
- Intended for high strength gray and nodular cast iron
- Seven sticks at a useful pack size
Cons
- Harder to machine than nickel-99 weld metal
- Requires preheat discipline on heavy sections
This is the companion to the Fox Alloy nickel-99 rod and the opposite choice. Where that one is specified for cast iron joined to itself and to steel with a soft, machinable deposit, this ENiFe-CI version is built for strength: the weld metal is described as stronger and more resistant to solidification cracking than other nickel electrodes.
It conforms to AWS A5.15 ENiFe-CI, EN ISO 1071 E C NiFe-CI 1 3 and GB/T10044 EZNiFe-1, comes as seven sticks at 12 inch by 3/32 inch, and is intended for repairing high-strength gray cast iron and nodular cast iron. The very good current-carrying capacity is the practical headline: this is a rod for thicker sections where a nickel-99 bead would need too many passes.
Where the extra strength pays off
Nodular and high-strength gray iron is where nickel-55 earns its place. These castings are stronger and less forgiving than ordinary gray iron, and a repair that merely matches the base metal can leave you with a crack that propagates around the weld instead of through it.
It is also a sensible choice when you expect the repaired part to see load or heat cycling. Seven sticks at 3/32 inch is a workable quantity for a serious repair, and the AC power source rating matches the small inverter or old transformer most home shops own.
Where it costs you
The trade is machinability. Nickel-iron deposits are harder to machine than nickel-99 weld metal, so if the repair is on a machined surface, budget real time for finishing or choose the softer rod instead.
Its 4.4 star average across 120 reviews with a 69 percent five-star share is the most spread of the strong performers – more four-star feedback than the nickel-99 rods. Reviewers treat it as the pick when strength and crack resistance matter more than a clean machining finish, and that is an honest way to use it.
6. HYW Products Nickel 99 Cast Iron Electrode – Easiest Arc to Learn On
Nickel 99 Cast Iron Welding Electrode Repair & Maintenance Rods (3/32″ – 5 PCS)
ENi-Cl 99% nickel
3/32 inch
5 piece pack
Excellent machinability
Suitable for production and repair
Pros
- Easy to start
- hot start and restart
- Good bead appearance that machines and files cleanly
- Reported to work on stainless to cast iron
- Five piece pack limits waste
Cons
- Some units arrive loosely wrapped with flux already shed
- Puddle can be hard to see while welding
- A minority of reviews report cracking soon after repair
The HYW nickel-99 rod is listed for both production and repair of cast iron, and its most useful feature is the deposit: excellent machinability of the finished weld. If the repair has to be trued back to a flat surface, this is the deposit you want to be able to cut.
What reviewers like most is the arc handling. Easy start, easy hot start and easy restart makes it beginner friendly in a way most nickel rods are not, and 4.4 stars across 110 reviews with 74 percent five-star is a comfortable score for a rod in this price and weight class.
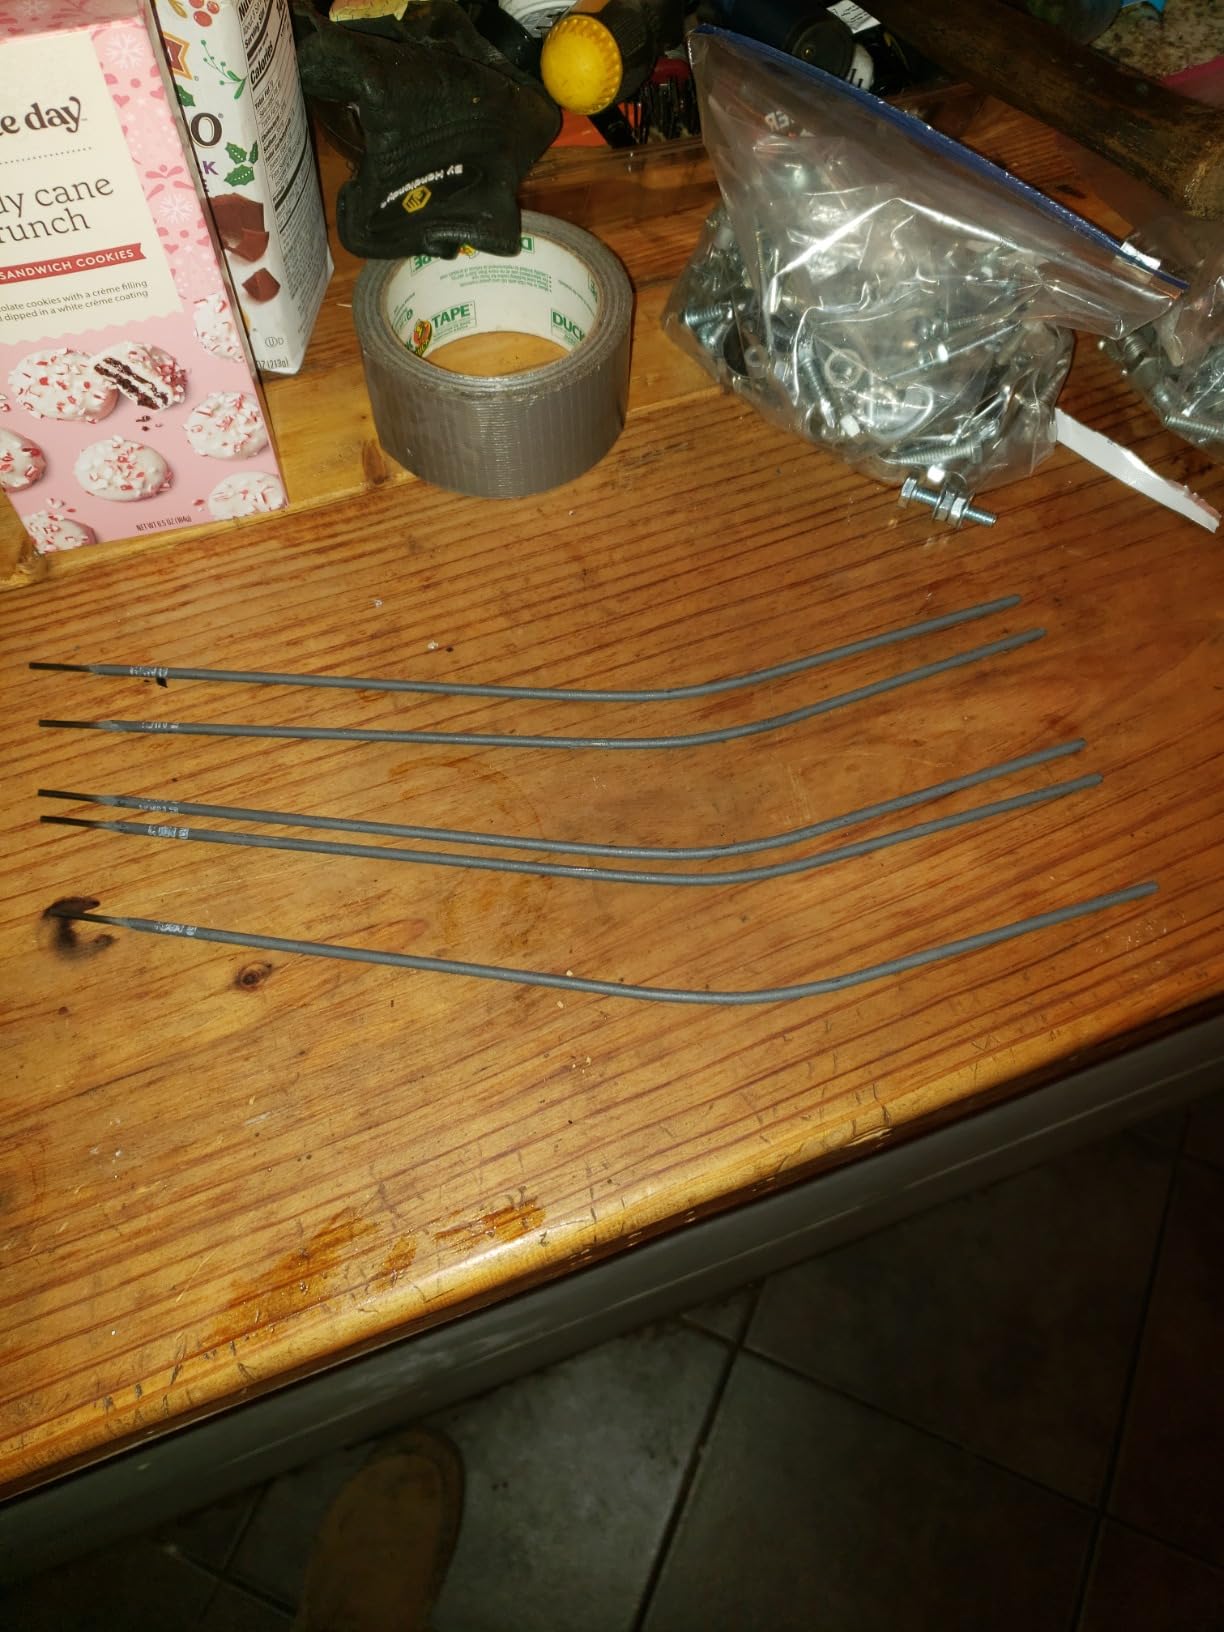
It is 3/32 inch diameter in a five piece pack, and the same product is offered in 1/8 inch and larger quantities, so the diameter is not a dead end if your first job turns out to be heavier metal. Reviewers also report it working on stainless to cast iron, which covers a lot of the cast-to-steel jobs that come up on farm and workshop repairs.
Why a beginner will do well with it
Cast iron punishes a hesitant welder, and this rod removes two of the usual beginner problems. It starts and restarts without fuss, so a mid-pass stop is not a crisis, and the deposit machines well, so a first attempt that comes out proud can be corrected instead of abandoned.
The five piece pack is the sensible entry size. It covers a single crack repair without turning leftover nickel rods into a moisture problem, and the small quantity keeps the cost of learning low.
What to watch for
Packaging is the main complaint. Some units arrive loosely wrapped with flux already shed from the rods, so inspect the sticks before you load them and keep the remainder sealed, because a damp coating is what causes porosity and weak beads.
There is also a small cluster of reports of cracking shortly after the repair, and reviewers note the puddle can be hard to see while welding. Cracking reports on any nickel rod almost always trace back to heat input or cooling rate, not the rod itself, so treat this as a reminder to preheat and slow the cool-down.
7. HYW Products Nickel 55 Cast Iron Electrode – Exhaust and Bell Housing Repairs
Nickel 55 Cast Iron Welding Electrode Repair & Maintenance Rods (1/8″ – 5 PCS)
ENiFe-CI 55% nickel
1/8 inch
5 piece pack
Surfacing and joining all cast iron grades
Nodular iron construction welding
Pros
- Excellent penetration with strong attractive welds on exhaust manifolds and bell housings
- Easy to strike and usable by non-professionals
- Machinable deposit with no post heat needed on test welds
- Performs competitively with dedicated cast iron rods
Cons
- Harder to machine than nickel-99 deposits
- Small number of one-star reports blaming material or equipment
This is the 1/8 inch version of the HYW nickel-55 rod, part of the ENiFe-CI family, supplied as a five piece pack. It is specified for surfacing and joining all grades of cast iron and for construction welding on nodular cast iron parts, so it covers both the repair and the build-up case.
The 1/8 inch diameter is the difference from the 3/32 inch rods elsewhere in this roundup, and it shows in practice. Reviewers highlight excellent penetration with strong, attractive welds on exhaust manifolds and bell housings, which are exactly the parts that want fill passes rather than single thin beads.
Several reviews mention striking an arc easily and welding cast iron cleanly as a non-professional, and testers report a machinable deposit with no pressure or post heat needed on test welds. It also sits at number 19 in Arc Welding Stick Electrodes, so it is a well-established listing rather than a new arrival.
Where it fits in a working garage
Exhaust manifolds and bell housings are heat-cycled parts, and this rod’s combination of penetration and a machinable deposit is the practical balance for them. The 4.4 star average across 84 reviews comes with a strongly positive spread – 69 percent five-star and 19 percent four-star – which is unusual for a welding consumable.
Because it is 55 percent nickel, it is also a sensible bridge material when you are joining cast iron to steel in the same repair, one of the situations that most often defeats a plain nickel-99 approach.
Where it does not suit
As with the other nickel-55 rods here, the deposit is harder to machine than nickel-99 weld metal. If the joint has to be faced off to a gasket surface or a bearing bore, choose the softer 99 percent nickel instead.
There is also a small tail of one-star reviews blaming the material or the equipment rather than the rod, which is the normal pattern when a product is bought by someone whose machine or preparation was not right. Buy the five sticks, do one practice bead on scrap, and judge it there.
8. Blue Demon Alloy 5000T TIG Rod – When You Want Minimal Preheat
Blue Demon BD-5000T-063-POP Cast Iron Repair
Alloy 5000T TIG rod
0.063 inch x 18 inch
AC or DC
Pop pack
Also in 0.094 inch
Pros
- Cast iron repair with minimal or no preheat
- Works on all cast irons
- Joins copper to steel and stainless
- AC and DC power source compatibility
Cons
- Not a stick electrode so it needs TIG equipment and different technique
- Most scattered rating in the group at 4.3 stars
The Blue Demon rod is the odd one out in this roundup, and that is exactly why it is here. It is a TIG filler, part number BD-5000T-063-POP, made from Alloy 5000T at 0.063 inch diameter and 18 inch length, working on either AC or DC. Everything else in this list is a stick electrode for SMAW.
The headline claim is cast iron repair with minimal or no preheat. That is a real process advantage. A TIG torch lets you walk the puddle along a crack slowly with a narrow bead, and slow welding on cast iron is exactly what buys you time to control heat input and avoid the tearing that shows up later.
Why a TIG rod earns a place in a cast iron list
If your machine is a TIG welder rather than a stick machine, this is your rod. It is specified as excellent for welding all cast irons, and it also welds copper to steel and stainless, so it covers more than the cast-to-cast case that most consumables are limited to.
The 0.063 inch diameter is the usual TIG filler size for cast iron work, giving fine control in tight areas, and the same rod is also offered in 0.094 inch if you want to put more metal down on a heavier joint. It comes in pop pack presentation, which is handy for keeping unused rod sealed.
Why it is not a universal pick
If all you own is a stick welder, this rod is useless to you – it needs TIG equipment, a foot pedal and a different technique than SMAW. The whole list above it works with a basic stick machine.
It also has the most scattered rating of the ten at 4.3 stars across 64 reviews, with 71 percent five-star and 7 percent one-star. The process advantage is real, but it is a narrower path than stick welding, and you need the right machine to use it.
9. Forney 43401 Nomacast Hard Cast Iron – Built for Dirty and Oxidized Metal
Forney 43401 Nomacast Hardcast Iron Specialty Rod, 1/8-Inch, 1-Pound
Nomacast hard cast iron specialty rod
1/8 inch x 1 lb
Non-conductive coating
Part 43401
90 day warranty
Pros
- Non-conductive coating designed for dirty heat affected and oxidized iron
- Clads contaminated castings before joining with nickel alloys
- Recognizable Forney brand
- 90 day manufacturer defect warranty
Cons
- Lowest average rating here at 4.2 stars with a 9% one-star share
- Smallest review base among the Forney entries at 42 reviews
Every nickel rod in this roundup assumes you have ground the casting back to clean metal. The Forney 43401 Nomacast is built for the cases where you cannot, using a non-conductive coating that is specified for dirty, heat-affected and oxidized cast iron.
That is a genuinely different job from the rest of this list. Old engine blocks, exhaust parts and castings that have sat outside for years carry oxides, sand and contamination trapped in the surface texture, and a conventional nickel electrode will simply refuse to wet them. The listing calls this rod great for welding dirty, heat affected and oxidized cast iron.
Where it is genuinely useful
The second application is the more interesting one. The rod is described as ideally suited to cladding contaminated castings prior to joining with high nickel alloys, which makes it a preparation step rather than a final answer – you clad the contaminated surface, then join it with a nickel-99 rod.
It is a 1/8 inch rod in a 1 lb package, model 43401, and it carries a 90 day warranty against manufacturer defects. Forney is a recognised name at the bench, and a warranty is something you rarely see on consumables.
Where it falls short
It has the lowest average rating of the ten at 4.2 stars across 42 reviews, with 9 percent one-star, and the smallest review base of the two Forney entries. A dirty-iron rod is a specialist tool, so a small reviewer pool is understandable, but it means you are trusting a narrower evidence base.
More importantly, cleaning is still better. Rods that tolerate contamination are a rescue for a casting you cannot strip, not a substitute for grinding back to sound metal, and using one as a shortcut means carrying the contamination into the finished repair.
10. Forney 45461 Super 55 Percent Nickel Rod – Shop-Grade Strength
Forney 45461 Super 55-Percent Nickel Cast Specialty Rod, 3/32-Inch, 1-Pound
55% nickel iron
3/32 inch x 1 lb
70000 PSI tensile
80 A capacity
Part 45461
Pros
- Dense hard and crack resistant welds stronger than nickel-99 deposits
- Sized for grade 30 40 and 50 gray cast iron
- All-position for repair and build-up
- 90 day manufacturer defect warranty
Cons
- Not easily machined and requires carbide tools
- Slowest-moving rod for a non-machining repair
The Forney 45461 is the heavy rod in this roundup. It is a 55 percent nickel iron cast specialty electrode at 3/32 inch in a 1 lb package, with a stated tensile strength of 70,000 PSI and an amperage capacity of 80 A. Those numbers put it in a different class from the small nickel-99 packs.
The weld is described as dense, hard and crack resistant, and the listing states plainly that these welds are stronger than Super Ni Cast 99 percent nickel welds. Typical applications given are grade 30, 40 and 50 gray cast iron, sewer pipe, machine bases, transmissions, gear housings and gear build-up – industrial work where strength and crack resistance outrank a clean machining finish.
The job it is built for
If you repair sewer pipe or a machine base and never put the joint back on a lathe, this is the right rod. It is an all-position electrode for repair and build-up, so it suits vertical and overhead work as much as flat, and the 80 A capacity means it is comfortable on a heavier machine than a small inverter.
It also carries a 90 day warranty against manufacturer defects and a listed dimensional specification meeting industry standards for comparable rods and amperage range, which matters when you are writing a procedure someone else has to repeat.
Why you probably do not need it
The stated drawback is not subtle: the weld is not easily machined and requires carbide tools. If the repair is on a machined surface, this rod will cost you tooling and time to get back to tolerance, and one of the nickel-99 picks is a far better tool for that work.
It also has the smallest review base of the ten at 40 reviews with a 4.2 star average and 65 percent five-star. A strong, well-specified rod for heavy industrial cast iron, but the most specialised choice here and the least necessary for a home workshop.
Buying Guide: Choosing the Right Cast Iron Welding Rod in 2026
55% nickel vs 99% nickel, which do you need?
The rule is simple. Choose 99% nickel when the joint has to be machined, drilled, tapped or faced afterwards. Choose 55% nickel-iron when crack resistance, penetration and load matter more than the finish on the deposit.
Nickel-99 gives the softer, more ductile deposit that files and mills easily, and it is the safer choice on thin sections and on parts you cannot fully stress relieve. Nickel-55 gives a harder, stronger weld metal with lower shrinkage stress and better resistance to solidification cracking, and it is specified for high-strength gray iron, nodular iron, sewer pipe and gear housings. There is a trade in both directions – a weld much stronger than the surrounding iron can itself stress and crack the casting, which is why machinability and ductility have real value.
What the AWS classification numbers actually mean
Most of the confusion in this category comes from not knowing what the code on the packet says. E Ni-CI is a nickel-iron electrode for cast iron, usually 99 percent nickel core, and it is the machinable choice. ENiFe-CI is the nickel-iron electrode at roughly 55 percent nickel and 45 percent iron, the strong and crack-resistant choice. ENiFe-C1 is the classified designation behind the common Ni-55 nickel-55 name, the same 55 percent nickel-iron family sold under a trade name.
You will also see European and Chinese equivalents on the same packets: EN ISO 1071 E C Ni-CI 1 and E C NiFe-CI 1 3, or GB/T10044 EZNi-1 and EZNiFe-1. They describe the same two alloy families under different standards bodies. If a listing states AWS A5.15 compliance, you know the rod was classified for cast iron work rather than being a generic nickel alloy.
Is the weld machinable? the question that decides most projects
This is the criterion that ruins the most repairs, and no editorial guide in this category states it plainly. If the repair sits on a machined surface and you cannot machine the deposit, you will destroy the part on a lathe or mill and start the job again.
Nickel-99 electrodes such as the Fox Alloy ENi-CI, SUA ENiCl, Weldcote Nickel 99 and HYW Nickel 99 are all described as machinable deposits. The 55 percent nickel-iron rods, including Forney 45461, are harder and less machinable, with the Forney specifying carbide tooling. Aluminum bronze products are the classic trap: easy to weld, but the deposit cuts like bronze and is not machinable in the way iron users expect.
My rule is to decide this before you buy anything. If the joint will ever touch a cutting tool, buy nickel-99. If it will not, buy nickel-55 and stop worrying about the finish.
Match the rod to your machine: stick, TIG or brazing
Almost everything in this roundup is a stick electrode for SMAW, and all of them work on AC or DC power sources, which means a basic stick machine is enough. Match diameter to the work: 3/32 inch rods suit thin sections, light fillets and controlled heat input, while 1/8 inch rods put more penetration down per pass on heavier castings and are the sensible choice for exhaust manifolds and bell housings.
If you run a TIG machine instead, a TIG filler rod like the Blue Demon Alloy 5000T is the correct consumable, and its minimal or no preheat capability suits controlled walking welds. MIG is rarely the answer for cast iron, and brazing with silicon bronze or aluminum bronze is a legitimate alternative when the joint is thin and you want lower heat input – many experienced users simply braze rather than weld when the part allows it.
Preheat, cool-down and surface preparation
No rod on this list fixes bad preparation. Grind the as-cast skin, sand, grit and oxides off the joint and a healthy margin around it, and get any coolant residue out of the pores. Then drill the ends of the crack so it cannot run further during the repair, and bevel or V-groove the joint so you are not trying to bridge a gap with a nickel bead.
Prewheat before welding – the Weldcote listing calls for roughly 300-450 F – and control interpass temperature so you are not building a heat sink in one area. Then let the part cool slowly, ideally under insulation or in clean dry sand, because cast iron tearing is a cooling problem. Stress relief after the weld is what stops an exhaust manifold repair from re-cracking on the first long drive.
Rod storage and moisture
Nickel electrodes are hygroscopic, which means they absorb moisture from the air and the coating spoils. Keep them sealed in the tube or a dry container between uses, store them somewhere dry rather than a damp shed, and if a pack has been open a long time, run a test bead on scrap before trusting it on the job.
This is why packaging complaints matter more than they look. Reviewers single out the sealed tube on the Weldcote pack and the sealed sleeve on the SUA product, and they single out loose wrapping on other rods as a genuine issue – a shed or damp coating is a direct route to porosity and a weak bead. If you have an unrelated project that involves cast iron cookware rather than repair work, our guides to cast iron skillets and cast iron griddles cover the cooking side of the material, and our cast iron cookware set roundup compares complete kitchens-worth of coated and bare pieces.
Frequently Asked Questions
What type of welding rod is best for cast iron welding?
A nickel-alloy electrode is the right answer: 99% nickel (E Ni-CI) for a deposit you can machine afterwards, or 55% nickel-iron (ENiFe-CI, Ni-55) for a harder, more crack-resistant weld on heavy or high-strength castings. Avoid mild steel rods – the weld shrinks with the casting and tears itself apart.
Can I use a 7018 welding rod on cast iron?
No. A 7018 is a low-hydrogen steel electrode with a yield strength the cast iron does not have, so it produces a rigid bead that the casting’s own shrinkage pulls apart as it cools. It will hold briefly and then crack at the heat-affected zone. Use a nickel or nickel-iron cast iron electrode instead.
What is the difference between Nickel 55 and nickel 99 electrodes?
Nickel 99 uses a nearly pure nickel core and gives a soft, ductile deposit that machines easily but has less crack resistance. Nickel 55 is about 55 percent nickel and 45 percent iron, giving a stronger, harder weld with lower shrinkage stress that resists solidification cracking but is harder to machine. Use nickel-99 on machined surfaces and nickel-55 on structural or heat-cycled parts.
What is the hardest welding rod to weld with?
Among cast iron consumables, 99% nickel electrodes are the most demanding – they want stable, low amperage and a steady puddle, and they punish a hesitant technique. 55% nickel-iron rods are more forgiving, and aluminum bronze products are the easiest but produce a non-machinable deposit. Skill matters more than the alloy in most failures.
Can you weld cast iron with a stick welder?
Yes. Every stick rod in this roundup runs on a basic SMAW machine with an AC or DC power source. The challenge is technique rather than equipment: grind the as-cast skin off completely, drill the crack ends, preheat to roughly 300-450 F, keep the puddle small and steady, and let the part cool slowly under insulation.
Conclusion: Best Welding Rods for Cast Iron Repair in 2026
The best welding rods for cast iron repair are the nickel and nickel-iron electrodes, and the pick we would buy first is the Weldcote Nickel 99 in 1/8 inch. It has the highest rating combined with the largest review base in the group, the most controllable puddle, a machinable deposit, and confirmed repairs on engine blocks, vises and manifolds.
Match the alloy to the job rather than the brand to the part. Nickel-99 for anything that will be machined or filed, nickel-55 for structural and heat-cycled work, the Blue Demon TIG rod if your machine is a TIG welder, and the Forney Nomacast when the casting is too dirty to strip properly. Whichever you choose, grind the casting back to clean metal, drill the crack ends, preheat and cool slowly – that preparation is what decides whether the repair holds.
Every rod above carries a Check Latest Price button so you can compare the current listing before you commit to a full pack.